Why Digital Work Instructions Depend on a Clean MES Connection
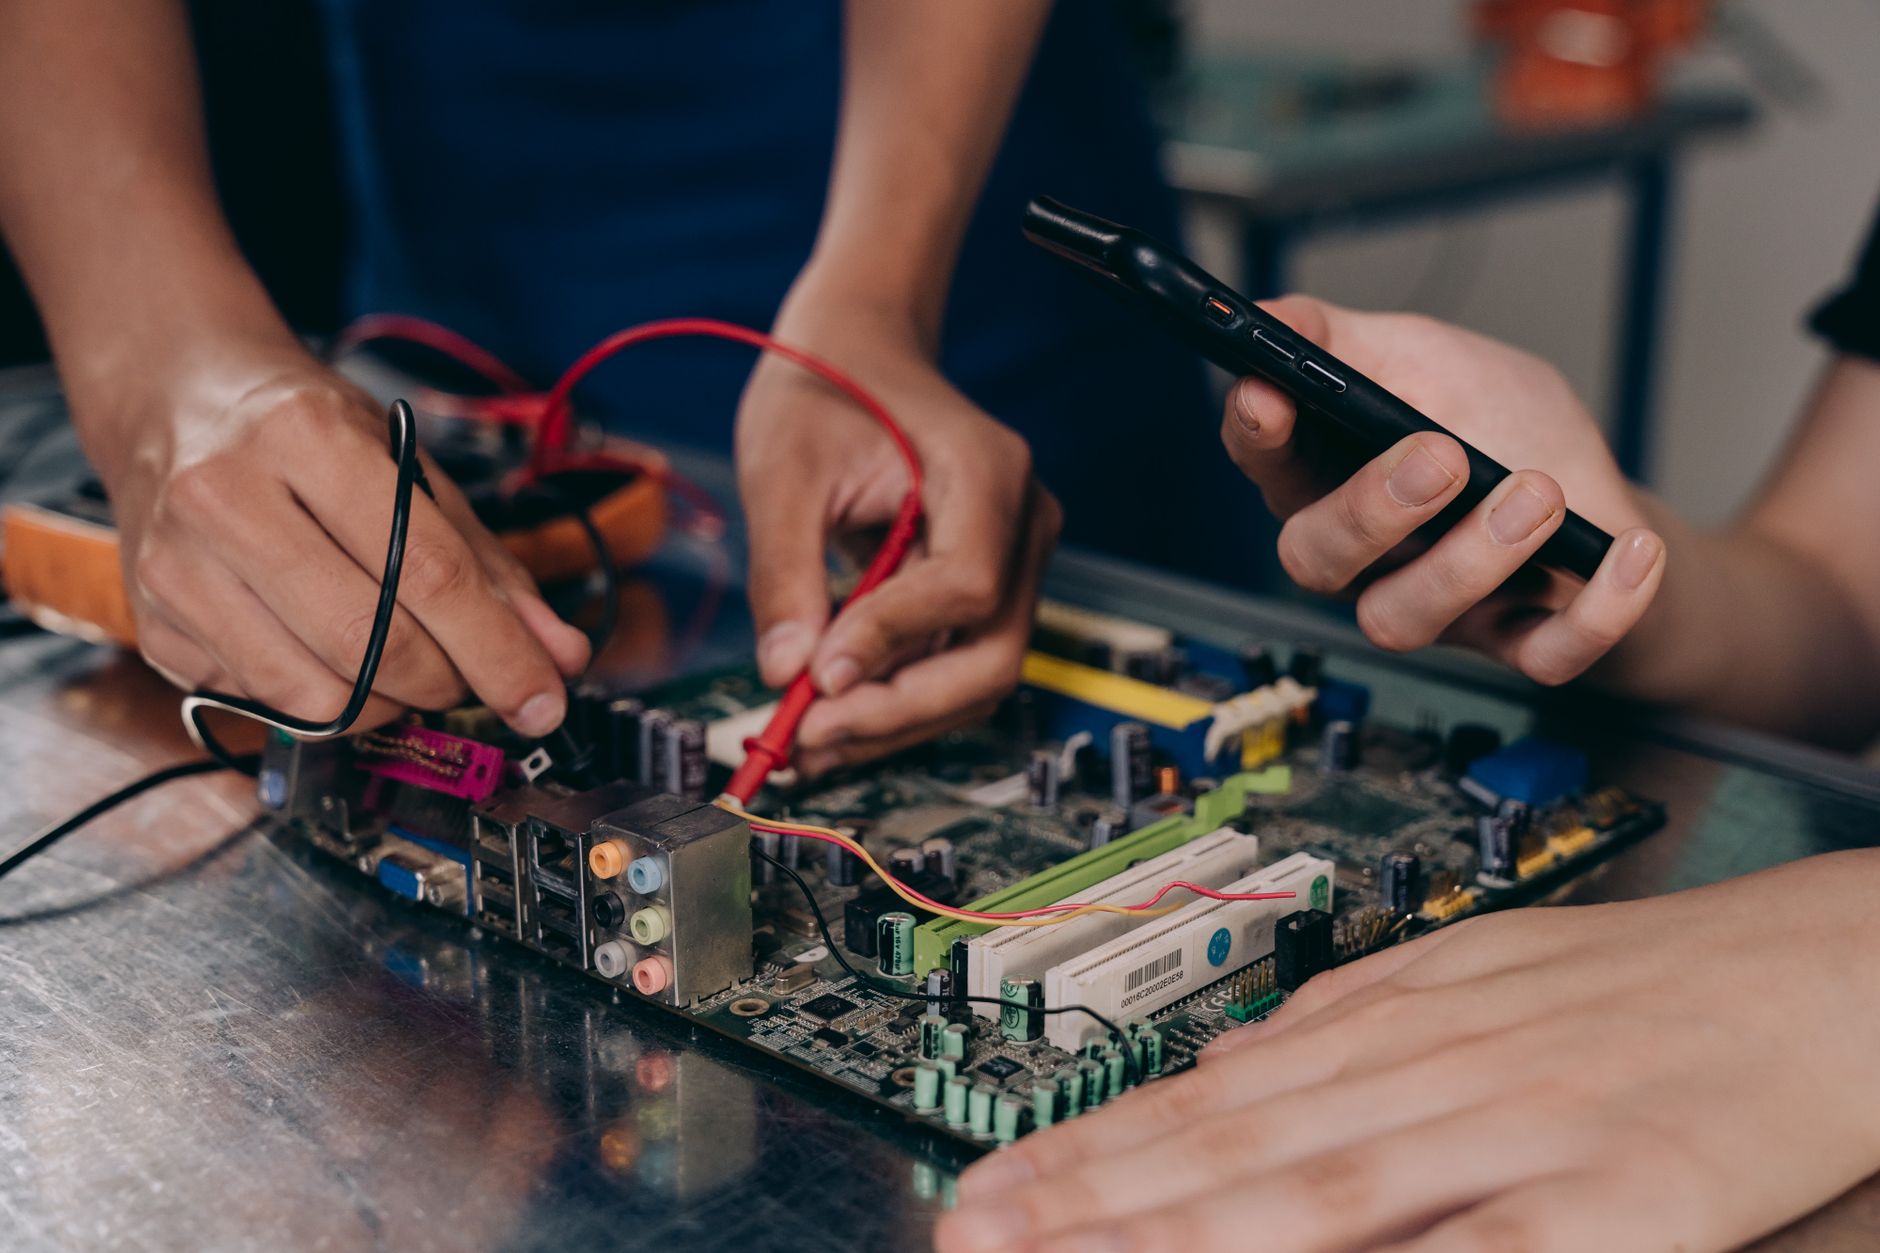
connected worker platform integration with mes systems is where many shop-floor projects either pay off or quietly stall. Putting work instructions on a tablet is the easy part. The harder part is making that screen know which order is running, which drawing revision applies, and where to send the results when the operator finishes.
Plenty of plants have digital instructions that look polished but still run on guesswork. An operator opens a PDF, types a lot number into a spreadsheet, and the MES never hears about it. Teams new to this topic often start with technical documentation and then realize the real problem is the data path, not the document.
Linking digital work instructions to an MES means the instruction screen receives job data, such as work order, part revision, and target quantity. When the operator finishes, completion records, quality results, and time stamps flow back. Most plants do this through the MES API, an OPC UA layer, or middleware, keeping the MES as the single record.
The MES sits in the middle of the plant’s information stack. The ISA-95 standard describes it as the layer between enterprise planning systems and plant control. That position is why the link matters. Instructions that ignore it can show the wrong step at the wrong time, and nobody notices until a batch is already off.
How Connected Worker Platform Integration With MES Systems Actually Works
Every working integration starts with a data map. You list what the instruction software needs from the MES and what it must send back. Then you match each item to a source field. This step looks dull, but most failed projects trace back to a sloppy map.
Mapping the Data Fields First
MES data models describe orders, operations, bills of material, and resources. The instruction software only needs a small subset. Typically that means the work order number, product code, routing step, drawing revision, quantity, and the ID of the equipment or tool in use. Match on IDs, not on display names, because names change and IDs usually don’t.
If your MES exposes data through OPC UA, field names come from the server’s address space. You can browse that space with a standard client tool and copy the exact node paths into your map. The OPC Unified Architecture specification explains how these nodes are structured. Write the map down before anyone writes code, and have a process engineer sign it off.
Dispatching Live Jobs to Operators
Dispatch is the moment the MES releases an operation to the floor. The platform should receive that release and show the instruction revision that matches it. If a revision changes mid-shift, the operator should see the new version on the next job, not a stale copy cached on the tablet. That rule sounds simple but it catches many teams off guard. A deeper treatment of this step lives at a deeper look for teams that need it.
There are two common ways to get the release. Polling asks the MES for updates on a timer. Event push lets the MES send a message the moment something changes. Push cuts the delay between release and display, but it needs the MES to support it. Polling interval is a tuning choice, so test a few settings on a single line before you commit. For the adjacent problem, Setting Up with Connected Worker Software for Automotive Assembly… goes deeper into the specifics.
Returning Completion Records to the MES
Completion data is what the MES actually cares about. That includes confirmed steps, measured readings, pass or fail results, operator ID, and timestamps. Send each record as a discrete transaction tied to the work order and operation. Avoid sending a single summary at shift end, because the MES loses the timing it needs for scheduling and traceability. The follow-up piece Which Connected Worker Tools for Mid Size Factories Fit the Budget? covers this in more practical detail.
In regulated plants, the return path carries extra weight. The FDA’s rules for electronic records and signatures in 21 CFR Part 11 apply to many of these transactions. The inspection results that come back from the floor follow the approach described at a deeper look, which is worth reading before you design that return path.
Handling Errors When the Connection Drops
Networks fail, and a shop floor will test your integration on a bad day. The instruction device should buffer completion records locally and resend them when the link returns. Give each transaction a unique ID so the MES can reject duplicates. Without that, a retry can book the same step twice.
Operators also need to see sync status. A small indicator showing pending records is enough for most teams. The harder decision is what happens to critical steps during an outage. Blocking production protects records but stops the line. Letting work continue keeps output moving but leaves gaps to reconcile later. Pick a rule per step and document it.
Two Illustrative Factory Scenarios for the MES Link
The following scenarios are hypothetical. They show how the pieces above fit together on a real floor, and they are not reports of specific customers.
A Torque-Critical Assembly Cell
Picture an assembly cell where each housing needs four bolts tightened in a fixed sequence. The MES releases the work order, and the instruction screen shows the current drawing revision and torque spec. Each bolt result returns to the MES with a timestamp and tool ID. When one result falls outside tolerance, the MES holds the unit for review, and the operator sees the hold reason on screen.
A Batch Step in a Food Plant
Now picture a mixing area where a recipe step needs a verified ingredient weight. The instruction screen pulls the batch record from the MES and blocks the next step until the weight is entered. If the network drops during the step, the entry is buffered locally. When the link returns, the MES receives it once, with a duplicate check stopping any double posting.
Testing the Link Before You Roll It Out Plant-Wide
Run the integration on one line for at least one full shift before expanding it. Replay a set of known work orders and confirm the right revisions appear. Pull the network cable on purpose and check that buffered records arrive once. These tests catch most of the problems that would otherwise show up during peak production.
Any connected worker platform integration with MES systems project benefits from a technical review before purchase orders go out. Comparing MES integration options against your own data map is a practical first step. If you want a second set of eyes on that map, the Vardian team offers technical consultations to walk through it with you.
Questions Plant Teams Ask About the MES Link
Do we need an MES that supports APIs before we can link work instructions?
Not always. Many older MES platforms expose data through database views, file exchanges, or an OPC server instead of a modern API. Each route works, but the latency and error handling differ. Start by checking what your MES already offers, then choose the integration method that matches it. Your IT team can usually confirm the options in an afternoon.
Who should own the data map between the MES and the instruction software?
Ownership works best when a process engineer and an IT lead share it. The engineer knows which fields matter on the floor, and the IT lead knows how the MES exposes them. Keep the map under version control so changes are visible. A shared document that nobody updates usually drifts within a few months.
What happens to digital instructions if the MES goes down for maintenance?
The instruction screen should keep showing the last released revision, clearly marked as cached. Operators can usually continue non-critical steps while completion records buffer locally. Critical steps may need a hold rule that pauses work until the MES returns. Document the rule per step so supervisors aren’t deciding it during an outage.
You May Also Like
- Automotive Plant Alert Escalation Using Connected Worker Tools
- Mobile Notifications Reach Supervisors Through Connected Worker Escalation
- Machine Downtime Alert Rules for Connected Worker Platforms
- Oil and Gas Teams Build Real-Time Escalation for Connected Worker Alerts
- Inspection Software Options for Automotive and Chemical Plants
Related Posts
Digital Work Instructions Explained for Factory Teams
Digital Work Instructions Explained for Factory TeamsPhoto: Gu Ko /…
Why operators ignore downtime alerts—and redesign industrial alert escalation system
Ignored downtime alerts are one of the most frustrating problems…
Layered process audit checklist items by layer
Why a Layered Checklist Keeps Operator Checks and Leadership Reviews…