Workflow design for connected worker success
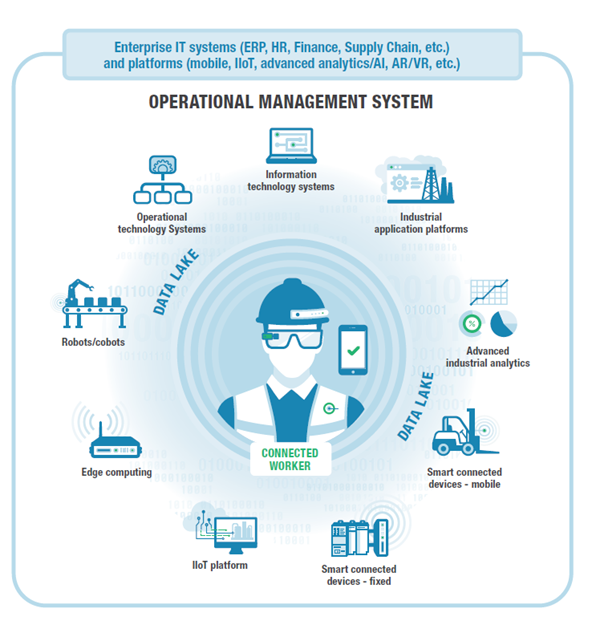
Workflow design decides whether connected worker manufacturing succeeds or stalls on the shop floor. Task clarity, clear exception routing, and defined ownership matter far more than any screen layout or mobile app polish. When frontline teams know exactly what finishes a task, who receives an alert when something goes wrong, and how information moves between roles. Adoption rises quickly and rework drops. Poorly mapped flows leave operators guessing, supervisors chasing updates, and data scattered across paper logs and disconnected spreadsheets.
connected worker manufacturing improves when the underlying logic matches real operations instead of generic software defaults. This article walks through the concrete decisions that turn a pilot into a stable system.
Effective connected worker manufacturing starts with mapping actual shift work in time-and-motion terms. Then build triggers and handoffs that match how teams already solve problems. The same logic applies whether the goal is maintenance, quality checks, or safety observations.
The Process, Step by Step
-
Map the current task in time-and-motion terms
Begin by watching how operators actually move through a task rather than relying on written procedures. Record start and finish times, travel distance between stations, tools required, and any waiting points. A time-and-motion study reveals hidden steps that never appear in standard work instructions. Most plants find that actual cycle time exceeds the documented version by 20 to 30 percent once walking, searching, and minor delays are counted. Use these observations to build the first digital version of the workflow inside the worker platform. The resulting map becomes the baseline against which later improvements are measured.
-
Define the “done” criteria for each task
Every task needs an unambiguous finish line that both the operator and the system recognize. Specify required data fields, photo evidence rules, or confirmation checkboxes before the task can be marked complete. Without clear criteria, tasks linger in open status and dashboards show misleading completion rates. In connected worker manufacturing, this step prevents the common failure mode where operators skip final entries because they believe the work is already finished. Test the criteria with two or three experienced workers before rollout. Adjust wording until everyone agrees the task is truly complete only when all fields are satisfied.
-
Create escalation triggers for missing parts, out-of-spec readings, and downtime signals
Decide in advance which conditions automatically notify the next role instead of waiting for manual reporting. Set thresholds for temperature, torque values, or part shortages that immediately open a follow-up task for maintenance or quality. Many connected worker platforms allow conditional logic that routes these alerts without extra configuration. Test each trigger during a short simulation so operators see exactly what happens when a reading falls outside limits. Clear triggers reduce the time between problem discovery and corrective action, which directly lowers unplanned downtime. The operational side is something Vardian connected worker manufacturing expands on with real numbers. This pairs well with Safety alerts via connected industrial worker from detection to…, which works through concrete examples. This pairs well with From detection to escalation via connected worker strategy, which works through concrete examples. For the adjacent problem, Connected worker inspection management comparison: point-of-work… goes deeper into the specifics.
-
Design handoffs between worker to supervisor, line to maintenance, and operator to quality
Explicit handoff points stop information from disappearing between shifts or departments. Define which fields transfer automatically and which require a human acknowledgment. For example, a quality flag created on the line should appear in the quality team queue with the original operator’s notes attached. In connected worker manufacturing, these structured transfers replace hallway conversations that never reach the system. Document the expected response time for each handoff so supervisors know when to intervene. Review the handoff matrix after the first pilot week and adjust ownership rules that prove unclear.
-
Choose the data captured at each workflow stage
Limit data collection to information that will actually be used for decisions or audits. Excessive fields slow operators and reduce compliance. Typical useful data includes part numbers, measurement values, tool IDs, and a short comment field for exceptions. Store photos only when they support traceability or training rather than capturing every step. Connected worker manufacturing programs that keep data lean see higher completion rates because operators spend less time on entry. Review captured fields quarterly and remove any that no longer drive reports or alerts.
-
Set governance rules for overrides and audits
Establish who may override a required field and under what conditions. Log every override with timestamp, reason, and approver so audits remain straightforward. Many facilities tie override rights to role levels inside the worker platform. Without governance, teams create workarounds that bypass safety or quality checks. Schedule a monthly review of override logs to spot recurring issues that need process changes rather than repeated exceptions. This step keeps the system trusted by both operators and compliance teams.
-
Pilot with one line and define success metrics tied to rework and downtime
Run the workflow on a single production line for four to six weeks. Track rework incidents, mean time to repair, and task completion time compared with the baseline map created in step one. Involve the same operators who helped define the flow so feedback stays grounded in daily reality. Success metrics should be visible on a shared dashboard updated at the end of each shift. If rework or downtime does not move, revisit the escalation triggers or handoff rules before expanding further.
-
Roll out by standardizing templates and training micro-content
Once the pilot proves stable, convert successful flows into reusable templates. Create short video clips or annotated screenshots that explain each step in under two minutes. Deliver this micro-content inside the worker platform so operators can review it on the floor rather than in a classroom. Connected worker manufacturing scales fastest when new lines inherit proven templates instead of starting from blank screens. Update templates only after the change passes the same pilot process used initially.
Defining exception categories early
Define an exception taxonomy early
Create a short list of exception types such as material shortage, equipment fault, or specification deviation before the first pilot shift. Operators then select from consistent categories instead of writing free text that later resists analysis. This simple step improves reporting accuracy across connected worker manufacturing deployments.
Use a single source of truth for task ownership
Assign each task type to one primary owner even when multiple roles participate. The owner receives the initial alert and decides when to escalate further. Ambiguous ownership is the fastest way for alerts to be ignored in any worker platform.
Schedule feedback sessions after the second pilot shift
Hold a brief stand-up meeting at the end of the second day rather than waiting until the pilot ends. Early adjustments prevent small frustrations from becoming habits. Frontline input at this stage often reveals handoff gaps that were invisible during planning.
Limit initial mobile fields to what fits on one screen
Keep the first version of any task form to five fields or fewer. Additional data can be added once operators demonstrate consistent completion. Overly long forms are the most common reason connected worker manufacturing pilots lose momentum in the first month.
Keep This in Mind
Workflow logic determines whether connected worker manufacturing delivers measurable gains or simply digitizes existing confusion. Validate every escalation path and handoff with the people who will use them before locking the configuration inside any worker platform. When frontline operators confirm the flow matches reality, adoption follows and the data becomes reliable enough to support continuous improvement.
Start with one clearly bounded process. Measure the results against rework and downtime. Then expand using the templates that worked. The same disciplined approach applies whether the site ultimately chooses connected worker platforms, connected worker software, or another connected worker solution.
- Parsable vs Redzone vs Hexagon for Connected Worker Manufacturing: Where Each Typically Fits
- When Corvex, Aveva, Honeywell, and SAP Overlap: Choosing by Manufacturing Outcome
- Connected Worker Platform Fit for Manufacturing Integrations: A Checklist for Data, Devices, and Governance
- Vendor-by-vendor Reality Check for Connected Worker Programs in Manufacturing
{“name”:”Designing a Connected Worker Workflow: From First Shift Tasks to Escalation Paths”,”step”:[{“name”:”Map the current task in time-and-motion terms Begin by watching how operators ac”,”text”:”Map the current task in time-and-motion terms Begin by watching how operators actually move through a task rather than relying on written procedures. Record start and finish times, travel distance between stations, tools required, and any waiting points. A time-and-motion study reveals hidden steps that never appear in standard work instructions. Most plants find that actual cycle time exceeds the documented version by 20 to 30 percent once walking, searching, and minor delays are counted. Use these observations to build the first digital version of the workflow inside the worker platform. The resulting map becomes the baseline against which later improvements are measured.”,”@type”:”HowToStep”,”position”:1},{“name”:”Define the “done” criteria for each task Every task needs an unambiguous finish “,”text”:”Define the “done” criteria for each task Every task needs an unambiguous finish line that both the operator and the system recognize. Specify required data fields, photo evidence rules, or confirmation checkboxes before the task can be marked complete. Without clear criteria, tasks linger in open status and dashboards show misleading completion rates. In connected worker manufacturing, this step prevents the common failure mode where operators skip final entries because they believe the work is already finished. Test the criteria with two or three experienced workers before rollout. Adjust wording until everyone agrees the task is truly complete only when all fields are satisfied.”,”@type”:”HowToStep”,”position”:2},{“name”:”Create escalation triggers for missing parts, out-of-spec readings, and downtime”,”text”:”Create escalation triggers for missing parts, out-of-spec readings, and downtime signals Decide in advance which conditions automatically notify the next role instead of waiting for manual reporting. Set thresholds for temperature, torque values, or part shortages that immediately open a follow-up task for maintenance or quality. Many connected worker platforms allow conditional logic that routes these alerts without extra configuration. Test each trigger during a short simulation so operators see exactly what happens when a reading falls outside limits. Clear triggers reduce the time between problem discovery and corrective action, which directly lowers unplanned downtime. The operational side is something Vardian connected worker manufacturing expands on with real numbers.”,”@type”:”HowToStep”,”position”:3},{“name”:”Design handoffs between worker to supervisor, line to maintenance, and operator “,”text”:”Design handoffs between worker to supervisor, line to maintenance, and operator to quality Explicit handoff points stop information from disappearing between shifts or departments. Define which fields transfer automatically and which require a human acknowledgment. For example, a quality flag created on the line should appear in the quality team queue with the original operator’s notes attached. In connected worker manufacturing, these structured transfers replace hallway conversations that never reach the system. Document the expected response time for each handoff so supervisors know when to intervene. Review the handoff matrix after the first pilot week and adjust ownership rules that prove unclear.”,”@type”:”HowToStep”,”position”:4},{“name”:”Choose the data captured at each workflow stage Limit data collection to informa”,”text”:”Choose the data captured at each workflow stage Limit data collection to information that will actually be used for decisions or audits. Excessive fields slow operators and reduce compliance. Typical useful data includes part numbers, measurement values, tool IDs, and a short comment field for exceptions. Store photos only when they support traceability or training rather than capturing every step. Connected worker manufacturing programs that keep data lean see higher completion rates because operators spend less time on entry. Review captured fields quarterly and remove any that no longer drive reports or alerts.”,”@type”:”HowToStep”,”position”:5},{“name”:”Set governance rules for overrides and audits Establish who may override a requi”,”text”:”Set governance rules for overrides and audits Establish who may override a required field and under what conditions. Log every override with timestamp, reason, and approver so audits remain straightforward. Many facilities tie override rights to role levels inside the worker platform. Without governance, teams create workarounds that bypass safety or quality checks. Schedule a monthly review of override logs to spot recurring issues that need process changes rather than repeated exceptions. This step keeps the system trusted by both operators and compliance teams.”,”@type”:”HowToStep”,”position”:6},{“name”:”Pilot with one line and define success metrics tied to rework and downtime Run t”,”text”:”Pilot with one line and define success metrics tied to rework and downtime Run the workflow on a single production line for four to six weeks. Track rework incidents, mean time to repair, and task completion time compared with the baseline map created in step one. Involve the same operators who helped define the flow so feedback stays grounded in daily reality. Success metrics should be visible on a shared dashboard updated at the end of each shift. If rework or downtime does not move, revisit the escalation triggers or handoff rules before expanding further.”,”@type”:”HowToStep”,”position”:7},{“name”:”Roll out by standardizing templates and training micro-content Once the pilot pr”,”text”:”Roll out by standardizing templates and training micro-content Once the pilot proves stable, convert successful flows into reusable templates. Create short video clips or annotated screenshots that explain each step in under two minutes. Deliver this micro-content inside the worker platform so operators can review it on the floor rather than in a classroom. Connected worker manufacturing scales fastest when new lines inherit proven templates instead of starting from blank screens. Update templates only after the change passes the same pilot process used initially.”,”@type”:”HowToStep”,”position”:8}],”@type”:”HowTo”,”@context”:”https://schema.org”}
Related Posts
Which value categories belong in your connected worker ROI model
Connected Worker ROI Models Need Clear Value Categories Connected Worker…
Connected worker evidence improves when SOP steps match shift and product runs: validation checklist
Connected worker evidence improves when SOP steps match shift and…
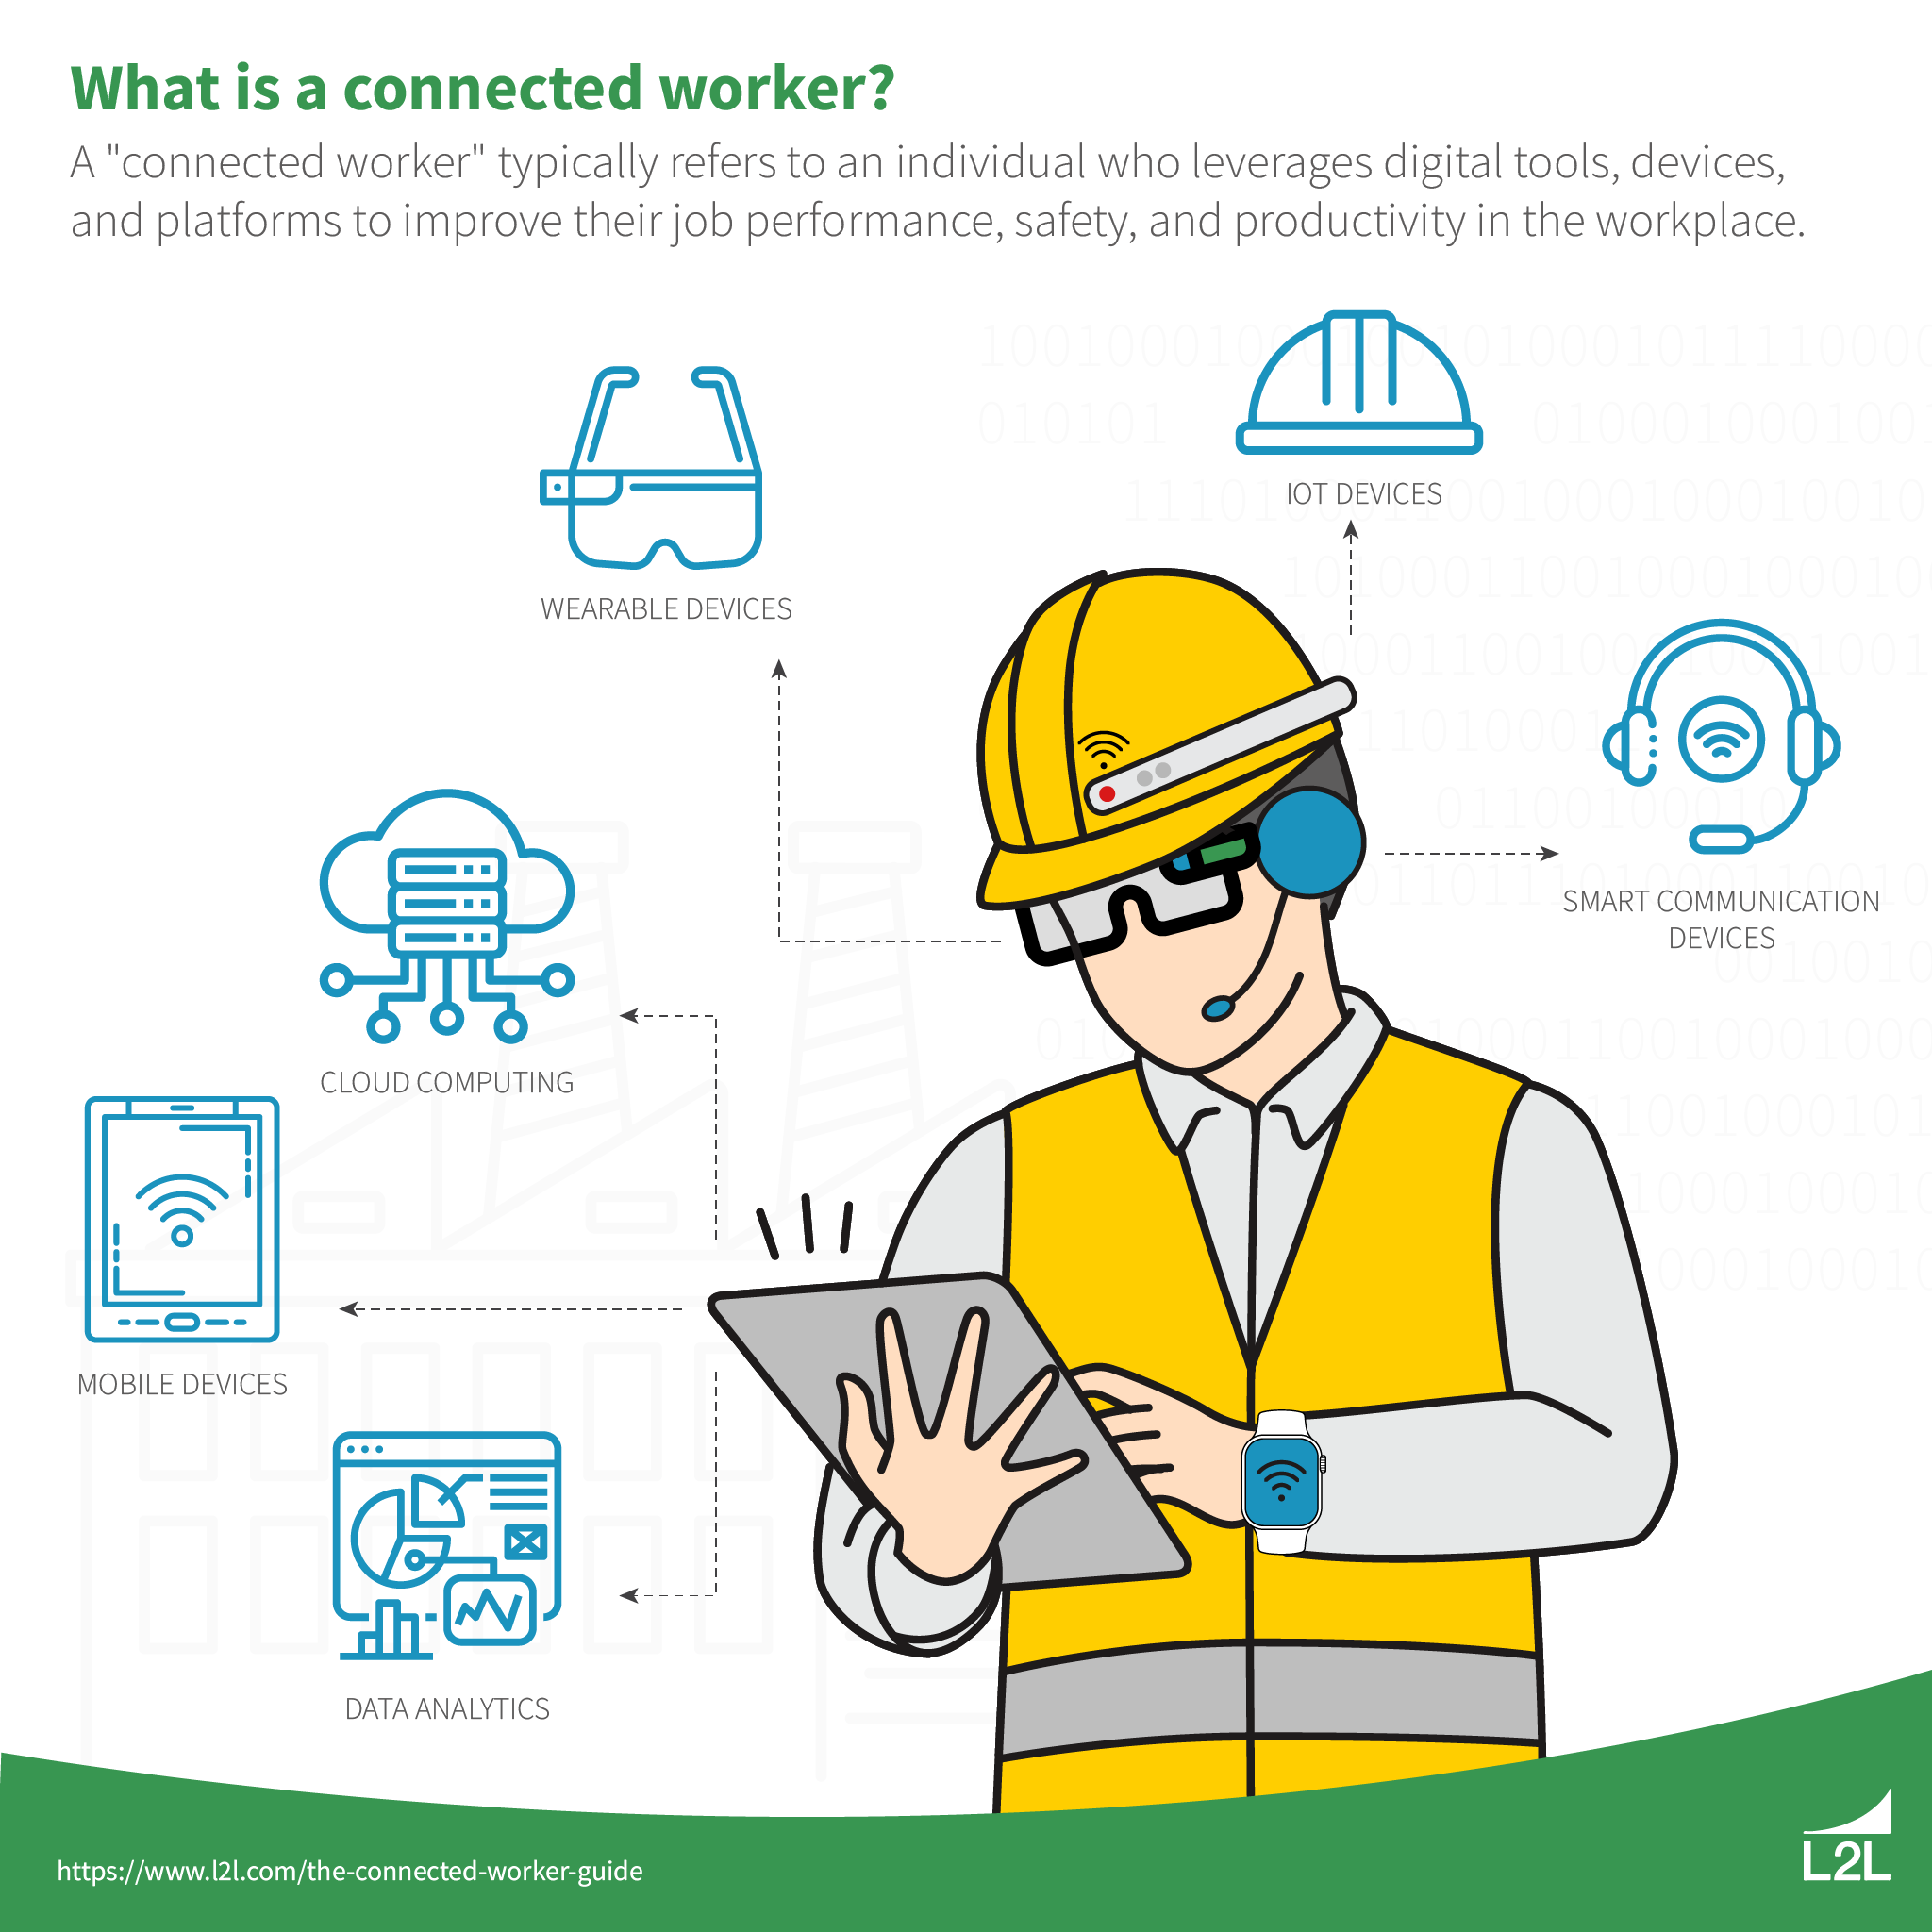
Implementing connected worker solutions: workflow design, integrations, and rollout sequencing
Workflow design for operational adoption Everything You Should Know About…